Graphite Components · TB-GR-MLD
Graphite Ingot Casting & Hot-Press Sintering Molds
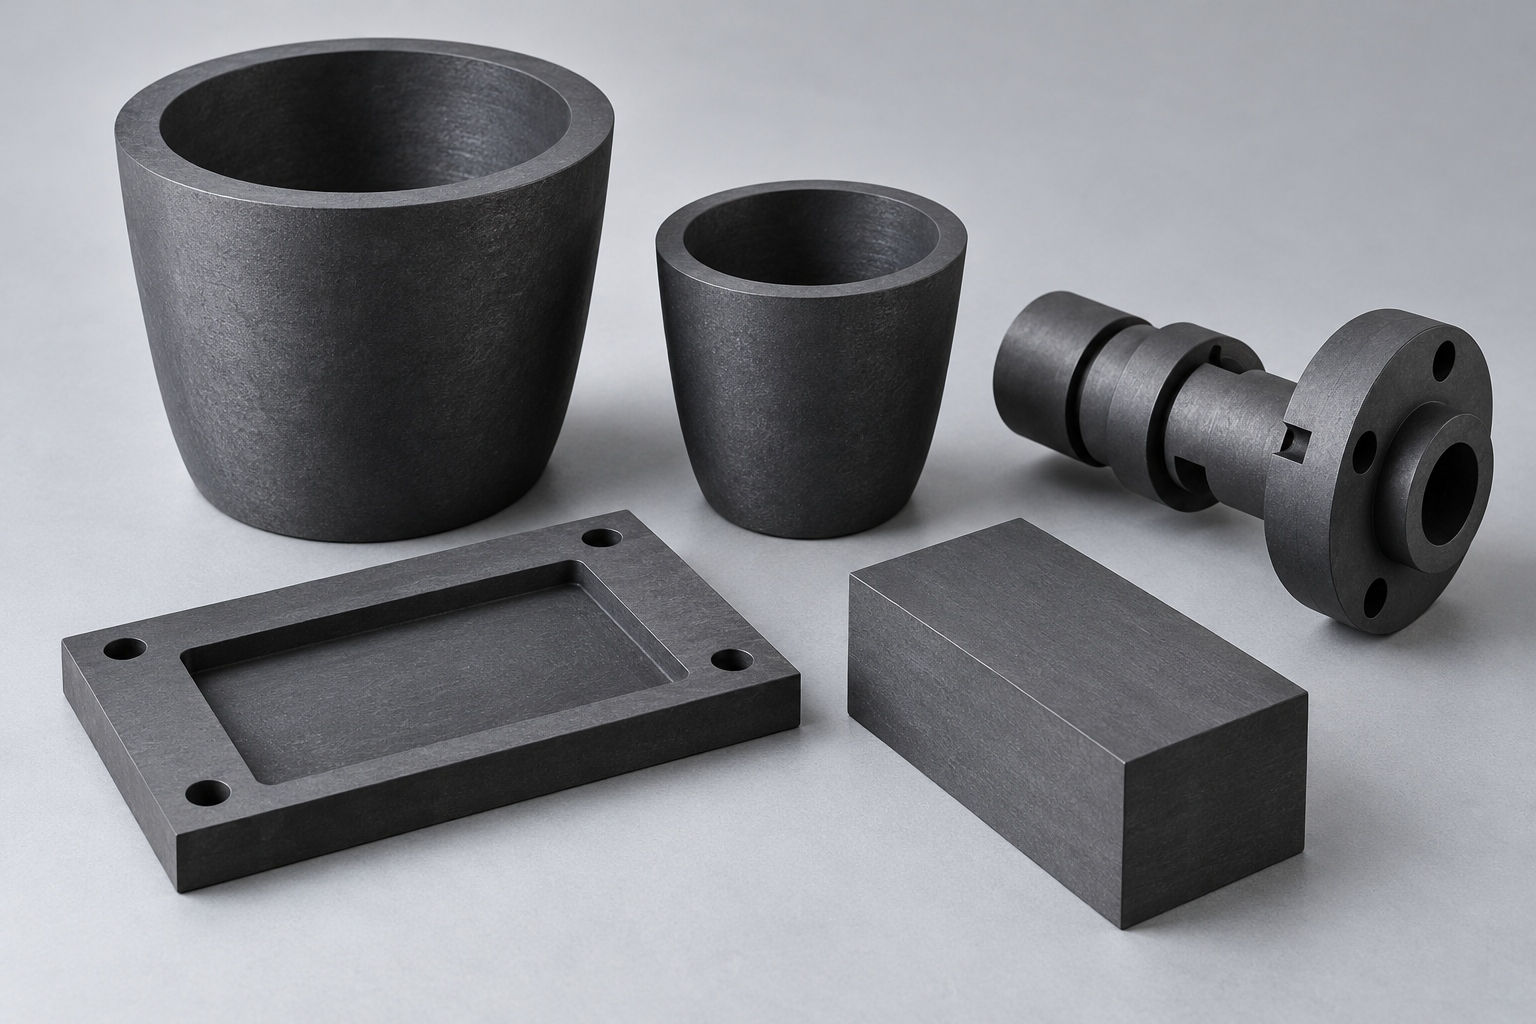
High-compressive-strength fine-grain graphite Spark Plasma Sintering (SPS) die/punch sets, hot-press sleeves, continuous casting dies, and polished ingot molds.
Alternate & search designations: Spark plasma sintering (SPS / FAST) graphite die & punch set, vacuum hot-press graphite sleeve, precious metal bar ingot mold, continuous casting graphite die
Purity / Grade OptionsHigh-Strength High-Density Isostatic Graphite (1.85–1.92 g/cm³)
Standard DimensionsIngot molds, continuous-casting dies, & SPS / Hot-Press die-punch sets
Available ConfigurationsSingle/multi-cavity ingot molds, split molds, SPS dies (Ø 10–100 mm ID) + punches
Ordering & MOQSpecification-based quote · Prototype & production lots
Material & Engineering Overview
Spark Plasma Sintering (SPS / FAST), uniaxial vacuum hot pressing, diamond-segment sintering, and continuous non-ferrous strip/rod casting push graphite to its mechanical limit under simultaneous uniaxial pressure (30–80 MPa) and high-current Joule heating up to 2,200 °C. Using high-strength ultra-fine isostatic graphite (compressive strength 110–150 MPa) maximizes clamping pressure ratings while delivering mirror-smooth cavity walls for clean part ejection.
We supply complete matched SPS die + upper/lower punch + spacer sets (plus flexible graphite foil liner rolls), split ingot molds, and continuous casting dies.
Standard Shipment Documentation: Manufacturer Mechanical & Physical Grade COA (compressive/flexural strength, resistivity, density, ash) and bore/punch clearance inspection.
Primary Research & Industrial Applications
- Spark Plasma Sintering (SPS / FAST) research & production die-and-punch tooling
- Uniaxial vacuum hot-pressing molds for ceramics, sputtering targets, and composites
- Continuous casting dies for OFHC copper, bronze, brass, and precious metal rod/strip
- Polished multi-cavity bullion, alloy button, and glass slumping molds
Nominal Material Reference Properties
| Property / Metric | Nominal Reference Value (Grade Dependent) |
|---|
| Compressive Strength | 105–155 MPa (high-strength SPS grade) |
| Flexural Strength | 55–85 MPa |
| Bulk Density | 1.84–1.92 g/cm³ |
| Typical Uniaxial SPS Pressure | Up to 50–80 MPa (geometry & wall-ratio dependent) |
| Cavity Surface Finish | Fine-turned / polished Ra 0.4–1.6 µm |
Reference values reflect typical sintered, fused, or wrought grades. Exact batch test figures are confirmed on your written quotation and accompanying lot Certificate of Analysis.
What to Specify in Your Quote Request
For SPS/hot-press sets, specify inner bore ID (e.g., 10, 15, 20, 25, 30, 50 mm), outer die OD, die height, punch length, punch-to-die diametral clearance (accounting for 0.15–0.2 mm flexible graphite foil if used!), thermocouple sight hole depth/diameter, and max uniaxial load.
Include target quantity, destination country/postal code for express air freight calculation, and any special cleanroom bagging or certification requests.
Prepare Graphite Ingot Casting & Hot-Press Sintering Molds RFQ ↗
Technical & Procurement FAQ
How much clearance should be machined between SPS punches and the graphite die bore?
When lining the bore with standard 0.2 mm (or 0.13 mm) flexible Grafoil paper, punches are typically turned 0.40–0.45 mm (or ~0.30 mm) smaller than the die ID so the foil slides smoothly without binding or powder extrusion.
Can you bundle flexible graphite foil (paper) and carbon felt sleeves with SPS die sets?
Yes—pre-cut flexible graphite foil sheets/discs and outer carbon-felt thermal jackets for SPS dies (to cut radiative heat loss above 1,200 °C) can be included on the same RFQ.
How do I prevent reactive ceramic/metal powders from carburizing against an SPS graphite punch?
Line the punch faces with h-BN spray, thin tungsten/molybdenum/tantalum barrier foils, or pyrolytic graphite discs—all available through Tensile Base.
 TB-GR-CR